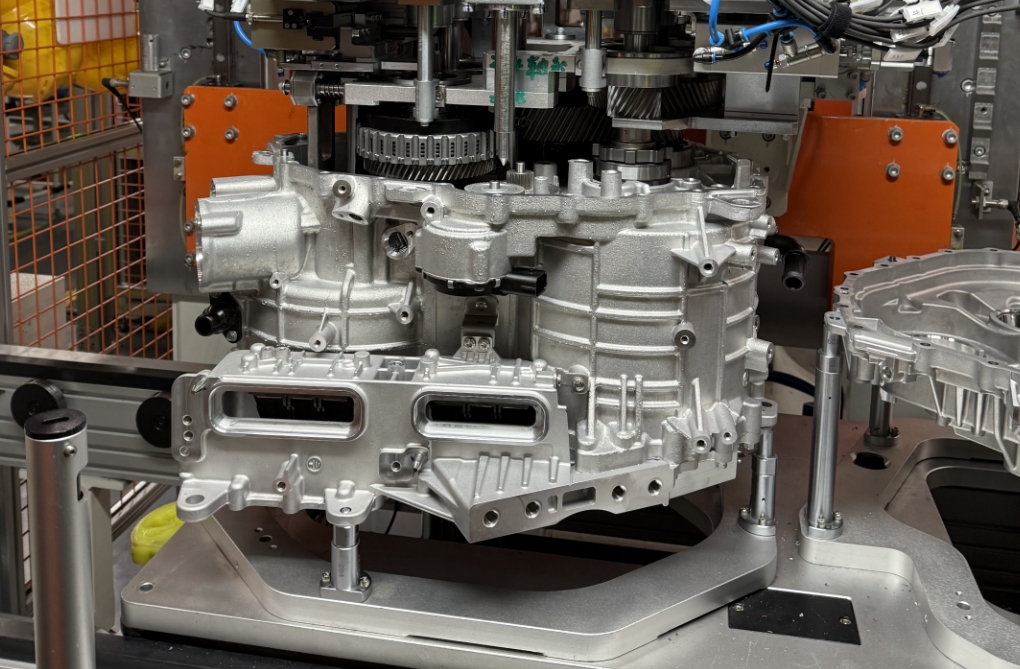
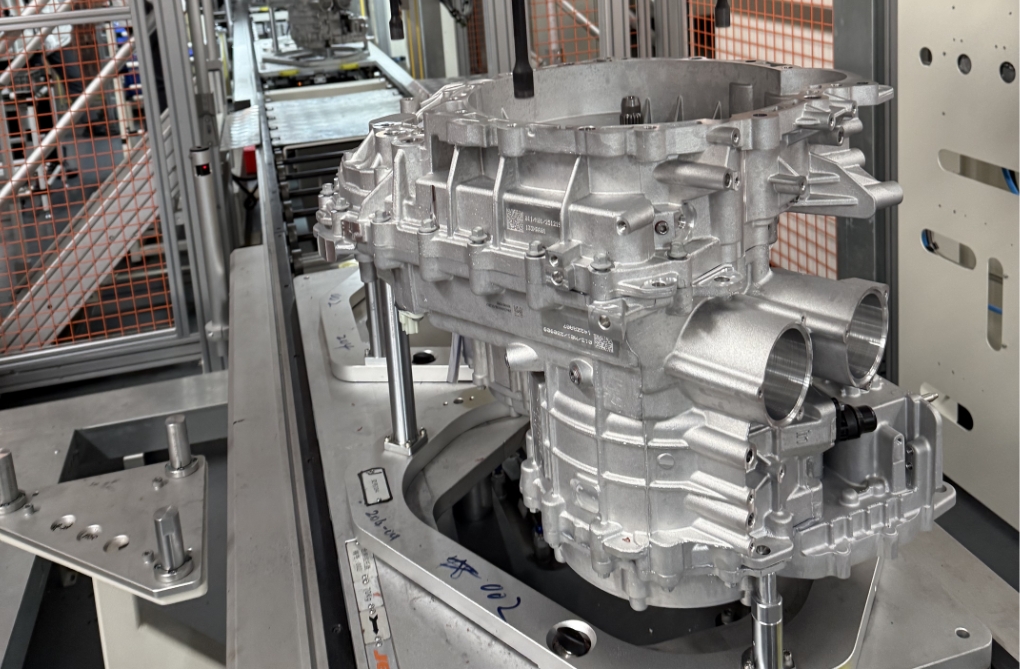
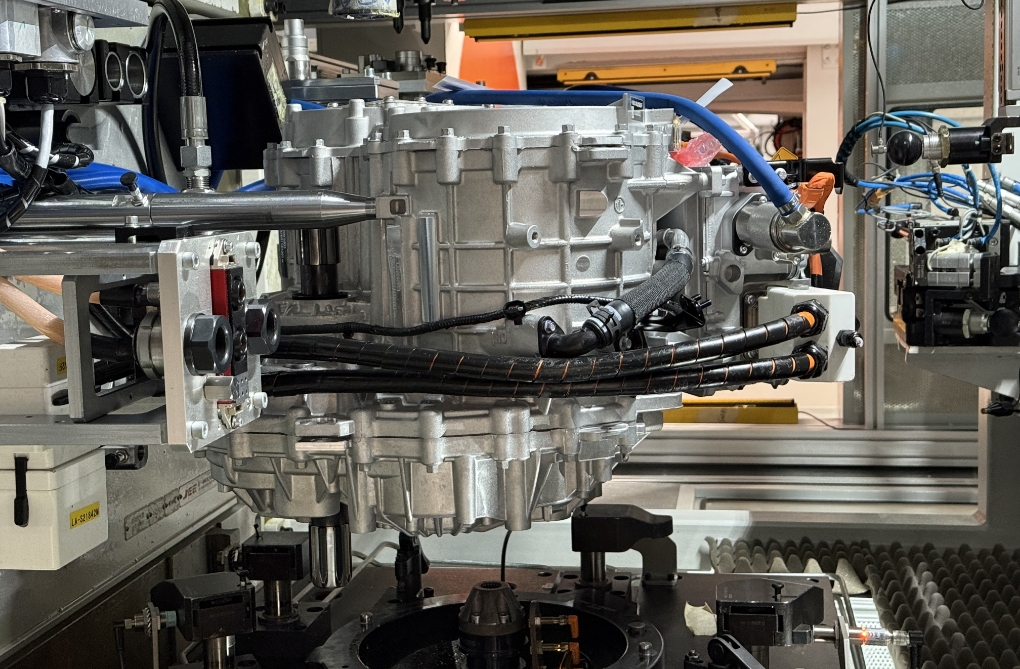
Jiangsu Transmission Plant
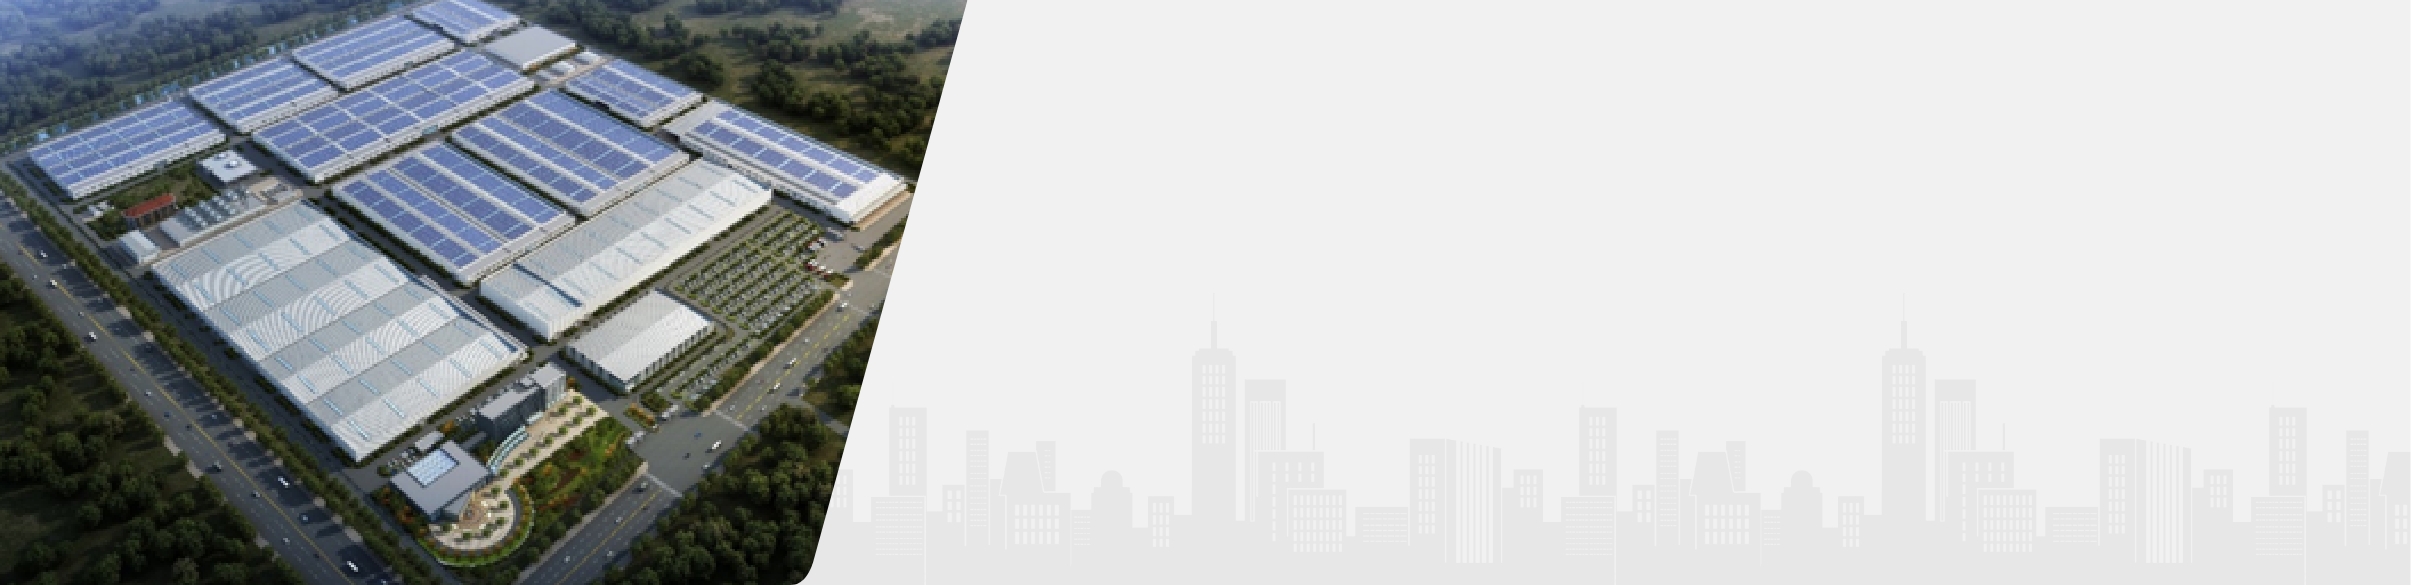
Located in Yangzhong, Zhenjiang City, Jiangsu Province, the plant was established in 2018, covering an area of 220,000 square meters.
It specializes in manufacturing core automotive components such as hybrid DHT transmissions and new energy drive motors. Its main products include DHT‑1, 9DCT, and 135 kW electric drive axle assemblies.
Since its launch, the plant has received numerous awards, many of its manufacturing processes are industry-leading.
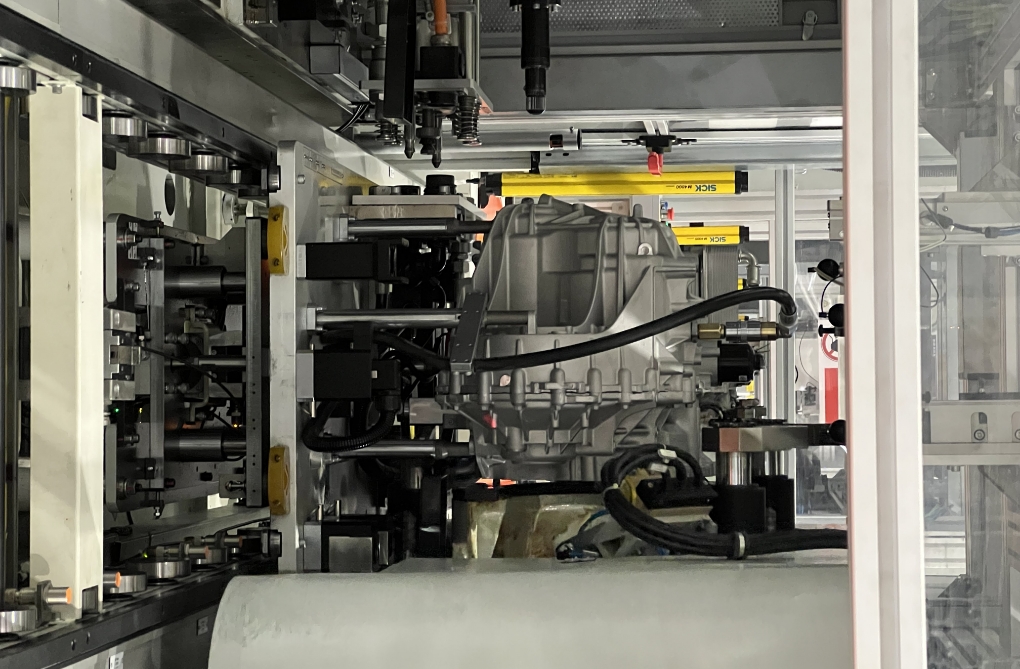
9(H)DCT Assembly Line
EOL Test
① Fully automatic test bench with availability over 95%.
② Integrated Siemens motors and HBM T12 high-precision sensors for full torque simulation.
③ Equipped with Discom ROTAS system for real-time NVH detection.
④ Integrated differential axle shafts and oil circulation control to improve uptime.
⑤ Test program with interlock and error-proofing functions.
⑥ Full performance test, real-time analysis and data recording for full lifecycle quality traceability.
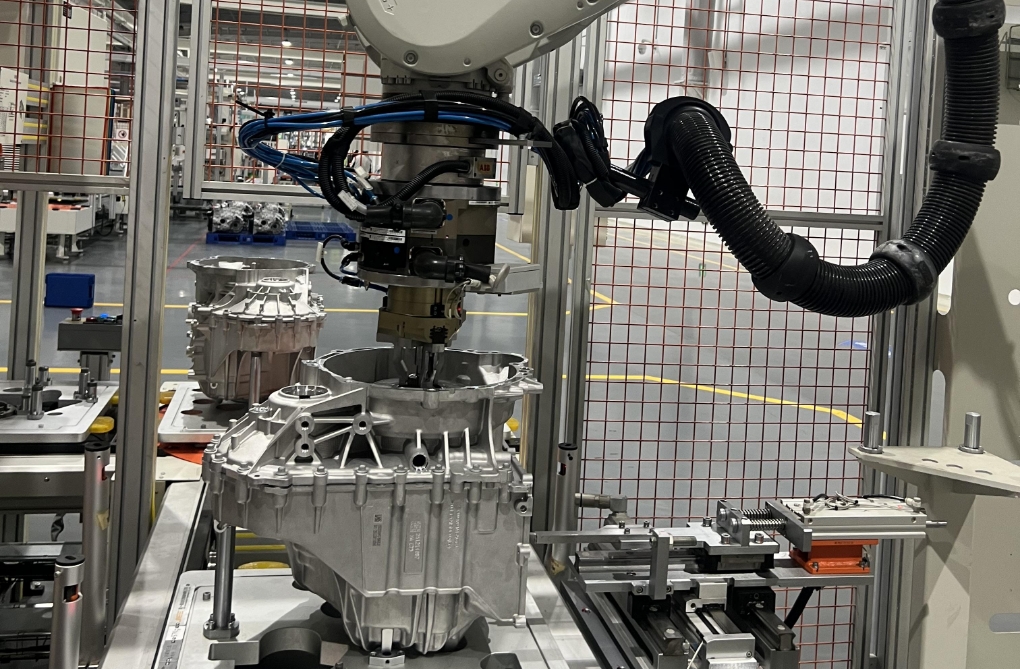
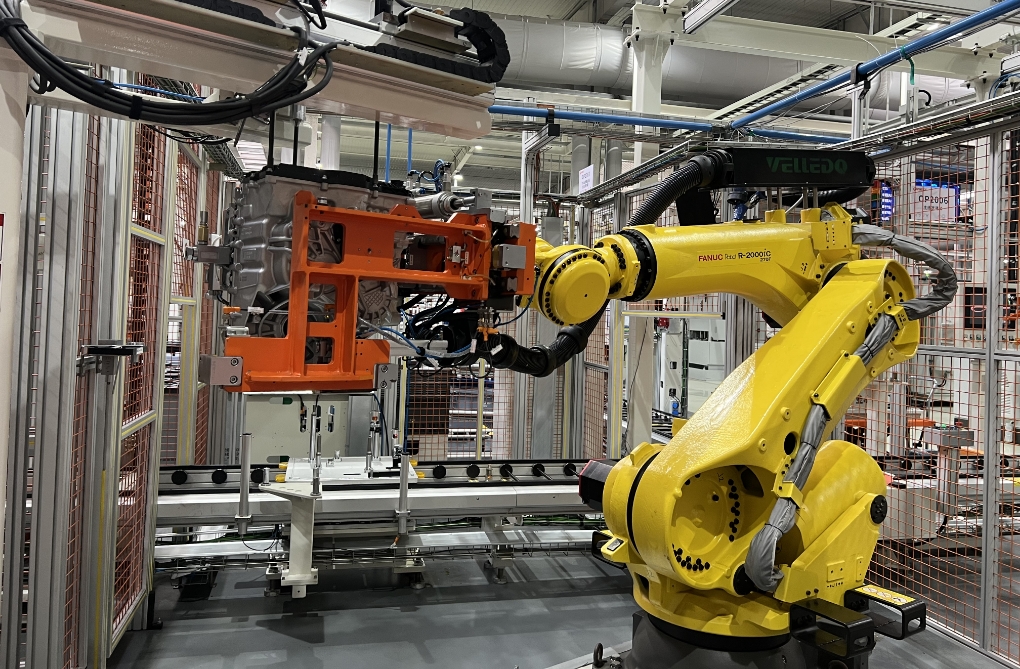
Assembly & Meshing
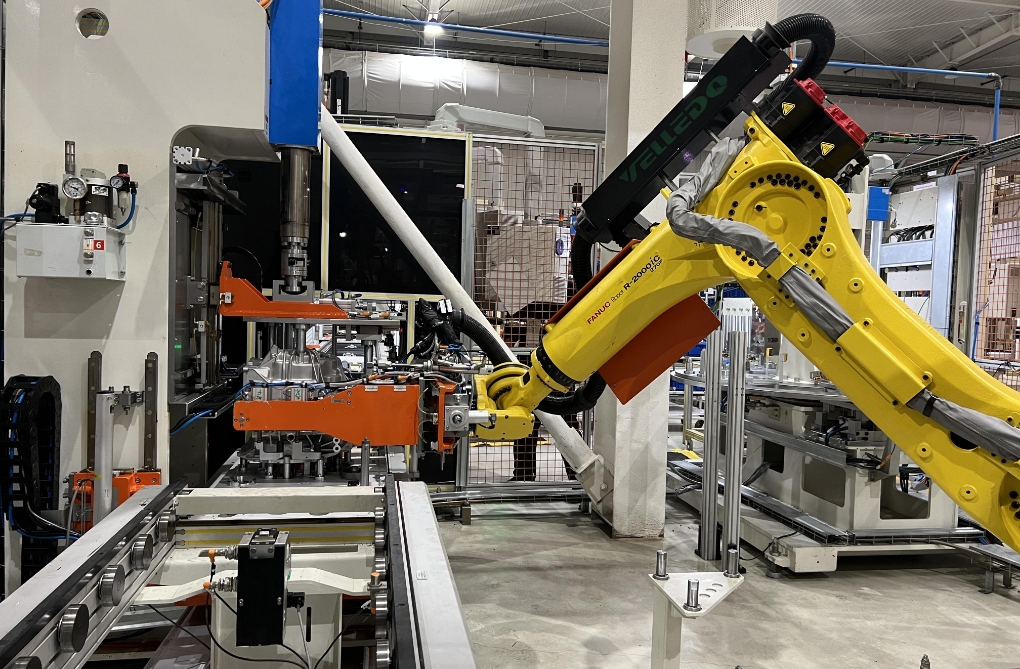
① Realizes clutch assembly & P2 motor assembly.
② Workstation operation: clutch assembly & P2 motor assembly.
③ Technology applied: robotics, force control technology, spline meshing.
④ Technical highlights: The robot automatically grasps the clutch and P2 motor, and realizes multi-stage spline automatic meshing through force control.
Cover Bolt Fastening & Assembly Line Transfer
① Adopts multi-axis bolt tightening and line transfer process.
② Workstation operation: Cover bolt tightening and assembly line transfer.
③ Technology applied: Robotic automatic tightening, handling and line transfer.
④ Technical highlights: Adopts fully automatic robotic multi-axis tightening technology to improve tightening quality. Automatic position adjustment enhances efficiency and flexibility. Integrated line transfer operation reduces costs.
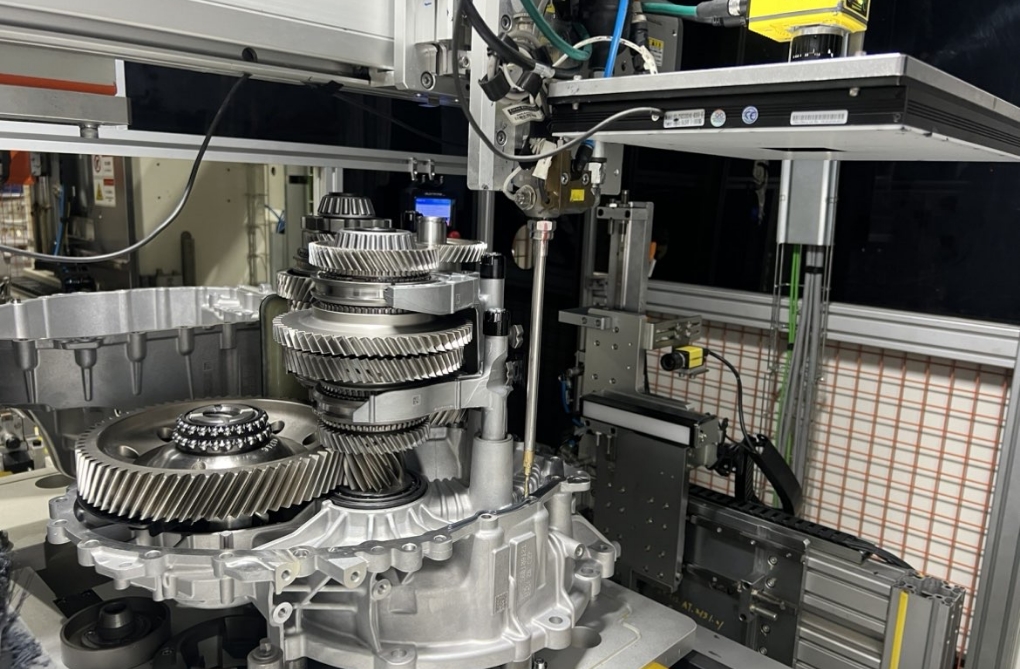
Adhesive Application & Inspection
① Adopts adhesive application and bead inspection process.
② Workstation operation: Housing adhesive application.
③ Technology applied: Servo-driven adhesive application, vision inspection + dark room.
④ Technical highlights: Equipped with X-Y servo slides for high-flexibility adhesive application, and conducts 100% visual inspection of adhesive beads to ensure bead quality.
Flexible Press-Fitting of Oil Seal Positioning Seat & Line Transfer
① Adopts flexible press-fitting of oil seal positioning seat and line transfer.
② Workstation operation: Housing adhesive application.
③ Technology applied: Servo-driven adhesive application, vision inspection + dark room.
④ Technical highlights: Equipped with X-Y servo slides for high-flexibility adhesive application, and conducts 100% visual inspection of adhesive beads to ensure bead quality.
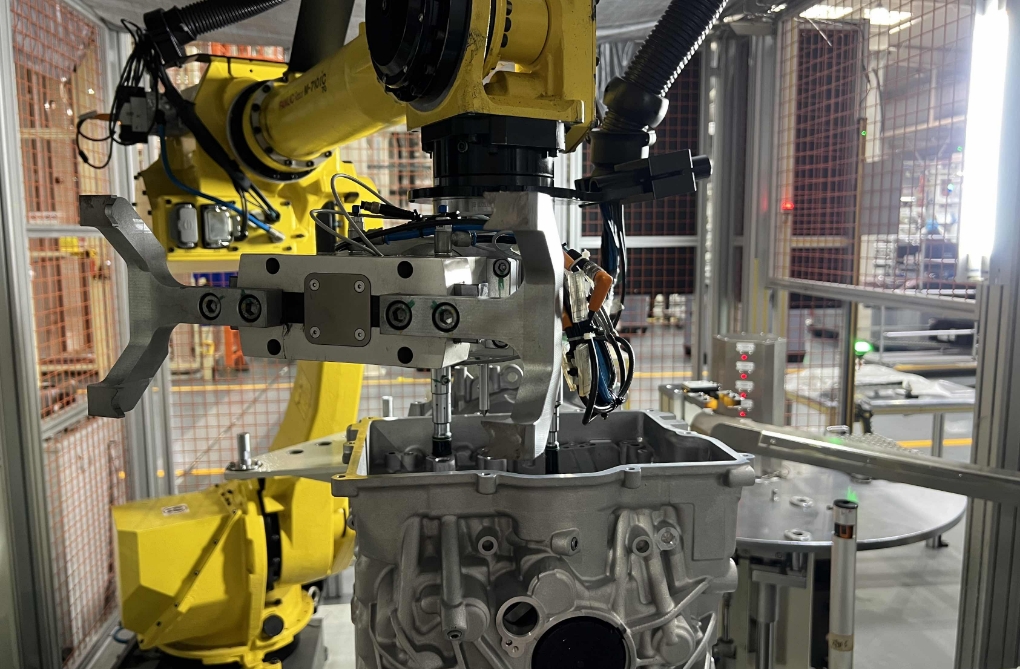
Flexible Press-Fitting of Oil Pipe
① Adopts flexible press-fitting process for oil pipes.
② Workstation operation: Flexible press-fitting of oil pipes.
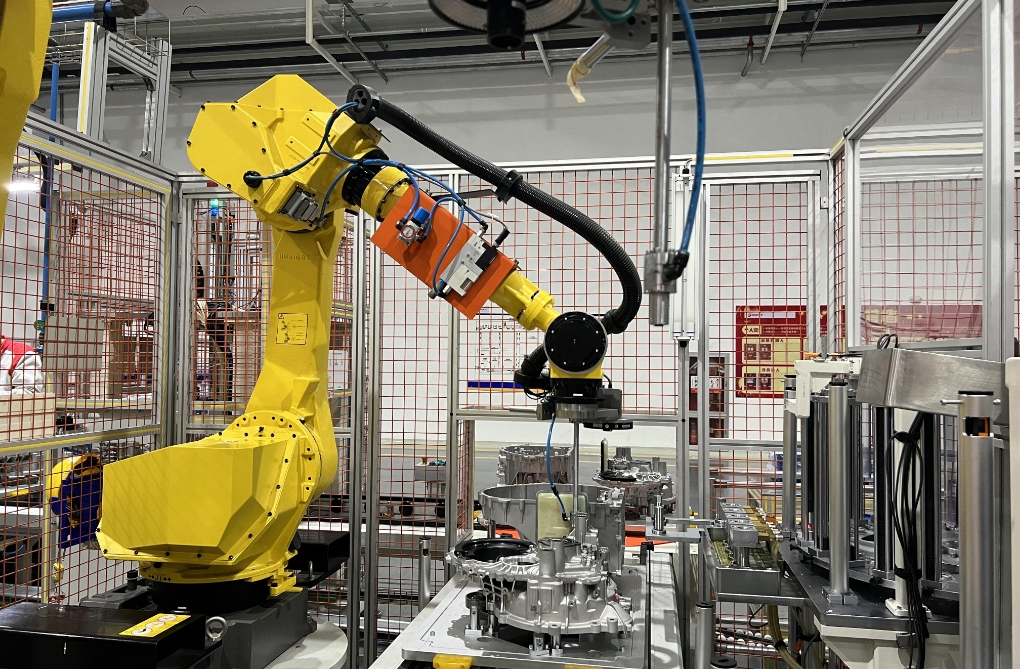
③ Technology applied: Robotics, oil coating, press-fitting, visual error-proofing.
④ Technical highlights: Vision-guided robot automatically picks up oil pipes, applies oil, and press-fits them in place. Visual inspection of press-fitting status ensures assembly quality.
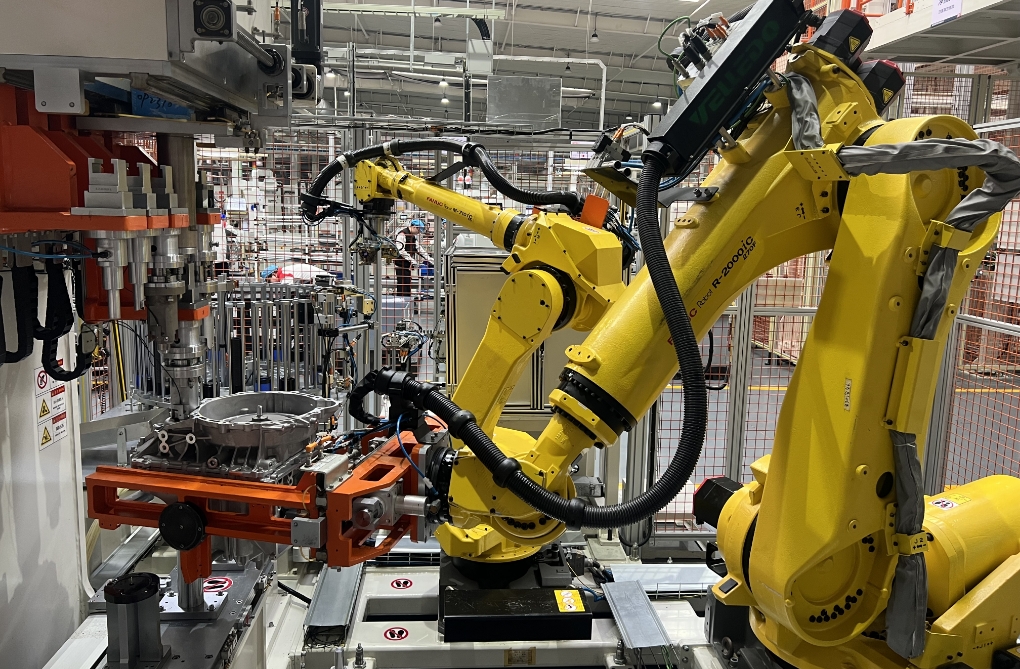
Housing Closing & Press-Fitting
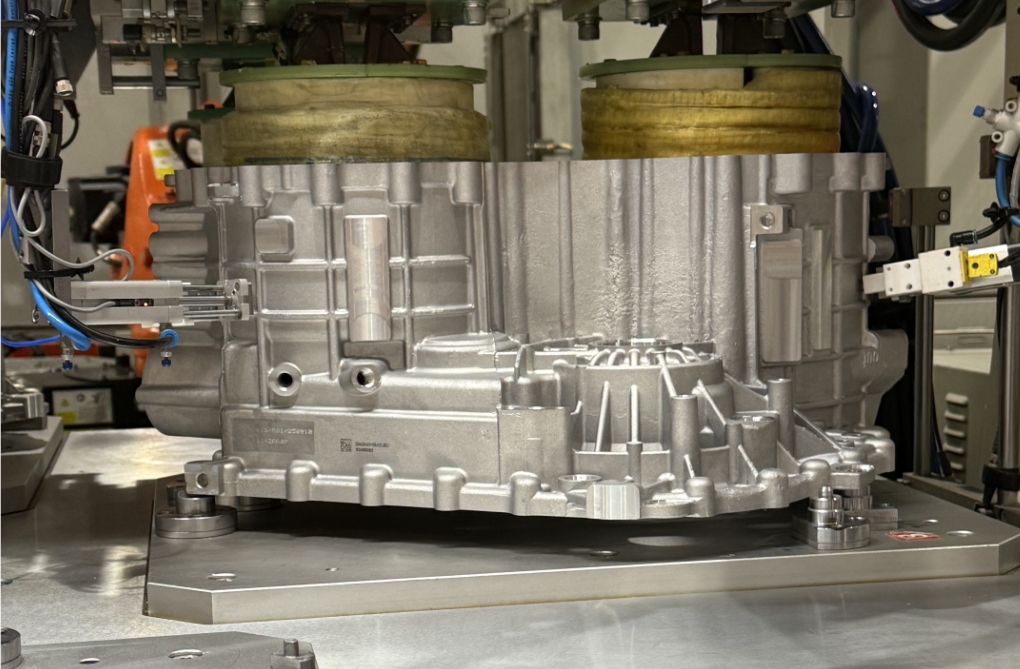
① Adopts housing press-fitting, adhesive application and housing closing processes.
② Workstation operation: Housing adhesive application and transmission case closing.
③ Technology applied: Robotics, adhesive application, multi-axis housing closing.
④ Technical highlights: The robot automatically grabs the housing, performs press-fitting and adhesive application, and realizes housing closing by adopting floating technology.
Fork & Piston Press-Fitting
① Adopts automatic assembly of fork and piston.
② Workstation operation: Automatic press-fitting of fork and piston.
③ Technology applied: Robotics, oil coating, press-fitting and visual error-proofing.
④ Technical highlights: Two robots automatically apply oil to the piston, press-fit it in place, and conduct visual inspection on the press-fitting status to ensure the assembly quality.
DHT1 Line
Armature shrink fitting
① Adopts dual-motor cavity heating process for the housing.
② Rigid-arm lifting + rotary table feeding, with one-drive-two split heaters for simultaneous cavity thermal expansion; robot completes dual-armature synchronous press-fitting and three-sided internal circulating air cooling, ensuring high flexibility, continuity and advanced industry level.
③ Applies robotic flexible heating-shrink-fitting and cooling technology, solving the industry problems of shrink-fitting stability and automation.
Housing press-fitting
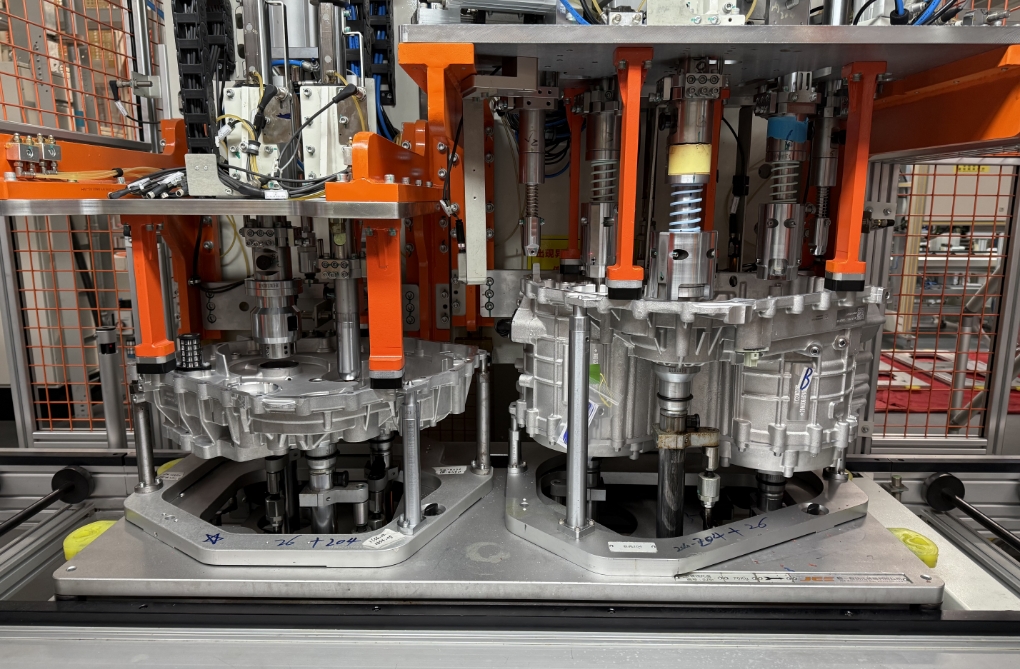
① The workpiece is gripped by the robot gripper and transferred to the slide table, which moves the housing to the press-fitting station for press-fitting. The robot then grips the workpiece again for transfer.
② The robot is equipped with a quick-change gripper assembly, the electric cylinder with a quick-change press head, and the slide table with a quick-change pallet assembly to enable rapid model switching. This greatly ensures precision, flexibility and compatibility, reaching an advanced level in the industry.
Shaft system measurement and splicing
At the station, materials are manually loaded and parts are delivered by the turntable. The handling robot grips the workpiece together with the gripper and moves it to the inspection station, where measurement is completed with a displacement sensor. The assembly robot then grips the workpiece together with the gripper and places it into the housing to finish assembly.
Robot tightening
At this station, the robot is equipped with an electric tightening spindle to perform automatic bolt tightening and automatic torque measurement, enabling rapid model switc.
EOL Test
① Final test for assembled assemblies to eliminate defects.
② Simulate actual operation with I/O mechanism, perform NVH test to verify assembly quality.
③ Display 1: motor speed-torque curve, clutch pressure, gear, voltage, current, speed, torque.
④ Display 2: vibration sensor energy diagram & motor speed-torque curve for NVH status.